CN | EN

Two quotations. Both read “CMC, DS 0.7, viscosity 800 mPa·s, 25 kg bags.” One is 18% cheaper. The real problem isn’t picking the cheap one — it’s that nothing on that line of text proves you’re being offered the same material.
Sodium carboxymethyl cellulose (CMC / Na-CMC, INS 466, E466) is the classic “the spec sheet looks simple, the material doesn’t be” excipient. It may be less than one percent of your formula, yet it decides whether a beverage synereses, whether an electrode slurry sheds powder, and whether a drilling mud stays inside its fluid-loss limit.
As a cellulose ether manufacturer, Fortune Biotech receives enquiries every day from buyers stuck on the same question: same published specs, so why does switching factories break the process?
This guide turns what we have seen go wrong into a practical evaluation method. It won’t tell you who is the best supplier. It will help you screen out the wrong ones in the first email exchange.
1. Don’t compare specs first — define the application
CMC is not one product. It is a family of grades whose priorities shift completely by end use. Quoting industrial-grade paperwork to a food project, or holding a general food-grade spec to a battery customer, are the most common mismatches we see.
| Application | Specs that actually matter | Typical trap |
|---|---|---|
| Food & beverage (stabiliser / thickener, E466) | Degree of substitution (DS), labelled viscosity, pH of a 1% solution, assay, glycolate residue, lead/arsenic and other heavy metals, microbial limits | “Technical grade” or “feed grade” wording used to pass off as food grade; documentation frozen on a withdrawn standard |
| Pharmaceutical excipient / personal care | Compliance with the relevant USP-NF, EP or FCC monograph, microbial limits, particle size and flowability, change control | Grade claims mixed across product lines; no written notification of formulation or process changes |
| Li-ion battery anode binder | DS (commonly 0.78–0.88 for graphite systems, higher for silicon-carbon), viscosity of a 1% solution, chloride / NaCl residue, iron and magnetic foreign matter, gel particle count, batch-to-batch variation | Incomplete washing leaves salt residue, which drives self-discharge and capacity fade |
| Drilling fluid / water-based mud treatment | Grade class (LV / MV / HV), active content, DS, API fluid loss, high-temperature stability | Inflated temperature ratings — short-term tolerance quoted as long-term resistance |
| Textile sizing, paper, ceramics, construction | Viscosity band, brightness, solution clarity, dispersion rate, salt tolerance | Low-clarity wood-pulp material sold into slots that need purified-cotton performance |
First step of any factory evaluation: send a half-page brief covering your application, your operating window (pH, temperature, salinity, shear, solids content) and your process (how you add it, agitation time, hydration/rest period, acceptance criteria). A competent supplier will ask follow-up questions. One that replies “yes we have that grade, price is…” can be moved to the bottom of the list.
2. Certifications: the certificate matters less than what it covers
A business licence, a production permit and an ISO 9001 frame are the entry ticket. These are the checks that actually eliminate half of your shortlist:
- Is the cited standard the current edition? This is the cheapest possible test of technical competence. Food-grade CMC in China is governed by GB 1886.232-2016, the national food safety standard for food additive sodium carboxymethyl cellulose, which superseded the withdrawn GB 1904-2005 on 1 January 2017. If a supplier’s COA or datasheet still cites GB 1904-2005, their technical documentation has not been maintained — and their internal QC practice deserves a broader second look. Industrial grades fall under chemical industry standard HG/T 5356-2018; export orders should map to FCC, USP-NF or EP monographs, or to an agreed and current in-house specification. (Figures quoted in this article are illustrative only; always confirm against the current text of the standard.)
- Does the scope cover your product line and the plant that actually ships? ISO 22000 certificates used to sell battery grade, a certificate holder that is not the manufacturing site, a scope worded “trading” rather than “manufacturing” — all of these exist. Ask for the certificate number and verify it on the issuing body’s register.
- The real bar for food-grade exports. For Middle East, Southeast Asian and Western food supply chains, Kosher, Halal and a GFSI-recognised food safety scheme are frequently hard requirements for customer approval and customs clearance. On Halal specifically, mutual-recognition scope differs by issuing body: for Indonesia confirm standing with BPJPH, for Malaysia JAKIM, for the Gulf the GSO 2055 framework. Holding a certificate is not the same as it working at your destination port.
- Completeness of the documentation pack: lot-specific COA, SDS/MSDS, statement of composition and process, TSE/BSE and allergen statements (food and pharma), non-GMO declaration, batch traceability records and a mock recall. Whether a supplier can produce this pack within 24 hours is itself a read on the factory’s management.
3. Look at the raw material route — it explains most of the price spread
The performance ceiling of CMC is set before etherification begins. When two factories are 20% apart on price, it is usually not who is greedier — it is that they are not starting from the same cotton.
| Raw material route | Cellulose purity | Achievable DP / viscosity range | Solution transmittance | Powder brightness | Best fit |
|---|---|---|---|---|---|
| Purified cotton (refined cotton linters) | ≥98%, alpha-cellulose ≥95% | High — covers high-viscosity grades | ~95%+, virtually no visible insolubles | ≥92%, minimal batch-to-batch colour drift | Food, pharma, battery and drilling-fluid grades |
| Cotton linters (not deeply refined) | ~90–95% | Medium — lower viscosity ceiling | ~85–92% | 82–88%, visible colour variation | Mid-range industrial; typically 15–20% cheaper than the purified-cotton route |
| Wood pulp | ~85–92%, with residual lignin and hemicellulose | Low — mostly medium to low viscosity | Generally <80%, tends to look hazy | 75–85%, may yellow in storage | Building materials, detergents and other clarity-insensitive uses |
Ask: “Purified cotton, cotton linters or wood pulp? What is your alpha-cellulose content?” Then check whether the answer and the quote are consistent. A supplier offering “full range, lowest price, wood pulp, high clarity” has just told you four things that cannot be true at once.
4. Look at the process — why “DS 0.7” is not enough information
Quotations nearly always state the average degree of substitution. What actually determines how the powder behaves in your tank is how uniformly substitution is distributed along the chain and across batches. That comes out of alkalisation and etherification control:
- Alkalisation uniformity sets the distribution of reactive sites — and largely explains unetherified fibre carryover, and a root cause of the fisheyes and gel particles that downstream users keep finding.
- Etherification dosing and temperature control governs DS distribution plus by-product carryover (glycolate, alcohol residues), which shows up as odour, pH drift and shelf-life behaviour.
- Washing and desalting sets chloride / NaCl residue. For battery and food customers this is a requirement, not a bonus.
- Drying and granulation set moisture, bulk density, dusting and — critically — dispersion on contact with water. Poorly granulated CMC of an identical formula hydrates on the outside and seals dry powder inside, which blocks spray nozzles and leaves white specks in the finished product.
- Line-clearance records for multi-product campaigns. A plant running dark industrial grade and white food grade on the same line must be able to show its changeover and cleaning records.
5. Look at the laboratory — in-house testing decides how fast a problem gets solved
Copy these questions straight into your audit:
- Can you test degree of substitution in house (acid-base titration or ash method, with blank correction)?
- How is viscosity measured — to the conditions written in the contract: concentration (1% or 2%), temperature (25 °C ± 0.1 °C in a thermostatic bath), spindle and RPM, and the rest period after preparation? Viscosity is highly sensitive to temperature and hydration time; a number without conditions is not comparable to anything.
- Can you measure clarity / insolubles (e.g. at 620 nm), ash, pH, loss on drying and chloride?
- For food and pharma, do you have heavy metal and microbiological capability?
- Are key instruments under calibration control, and is the lab actually running samples today?
A factory without in-house testing has handed your quality judgement to its own supplier.
Three quick screens for adulteration are worth remembering: abnormally high ash with dark residue after ignition (inert salt filler), unusual flocculation in a 95% ethanol precipitation test (starch or dextrin cutting), and a measured viscosity more than ±10% off label when retested under the contracted conditions.
6. Look at batch consistency, not one flattering COA
A single good batch may simply be a selected sample. Make the request explicit: please provide original COA data for three to five consecutive lots of the same grade, and plot the key parameters as a trend.
Well-controlled plants typically hold lot-to-lot variation within ±10% on viscosity and ±0.05 on DS, with gel particle counts judged against an agreed limit. A supplier willing to release consecutive-lot data usually has process capability to show for it. One that offers only “Typical values” and refuses lot actuals has already answered a question for you.
At the same time, agree incoming acceptance criteria and an arbitration test method before the first shipment. Write the sampling plan into the contract: treat one lot of one grade as one sampling unit; for lots up to 50 bags take 5 bags at random, then one additional bag per 10 bags beyond that; sample from the top, middle and bottom of each bag, blend and reduce by quartering to no less than 500 g, seal in two equal portions — one for testing, one retained for at least three months for dispute traceability.
7. Look at trials and technical service — that’s what you need on the bad day
This is where suppliers truly separate:
- Do they offer sample support with a defined trial protocol (addition sequence, agitation speed, water temperature, hydration time, pass/fail criteria)?
- Will someone attend the first plant trial, or analyse a sample of your out-of-spec material before you stop production?
- When something goes wrong, do they come back within a committed timeframe with retained-sample retest results, root cause and corrective action — rather than “we’ll send you good material next time”?
A reliable rule of thumb: the supplier who wants to discuss the test method before the price is usually worth your time.
8. Look at capacity and delivery reality
- Nameplate annual capacity versus current backlog determines whether your volume is genuinely welcome.
- Is there stock of the regular grades — a 7–15 day lead time versus 45 days will be exposed at peak season.
- Does the plant depend on a single raw material source that can move price or force a formulation change?
- Packaging and protection: 25 kg bags with PE liner, fibre drum or FIBC. CMC is hygroscopic — damaged liners and container sweat turn good powder into a pallet of blocks.
- Export maturity: can they explain documents (commercial invoice, packing list, Certificate of Origin, Health Certificate / Free Sale Certificate), booking and transit time without hesitation?
9. Ten minutes on the factory floor tells you more than the showroom
Whether on site or by video audit, look here first:
| Where to look | Good sign | Warning sign |
|---|---|---|
| Raw material yard | Segregated, lot-labelled, protected from moisture | Mixed piles, no labelling, noticeable odour |
| Production area | Separated people/material flows, contained dust, cleaning records on hand | Dark-to-white changeover with no documented segregation |
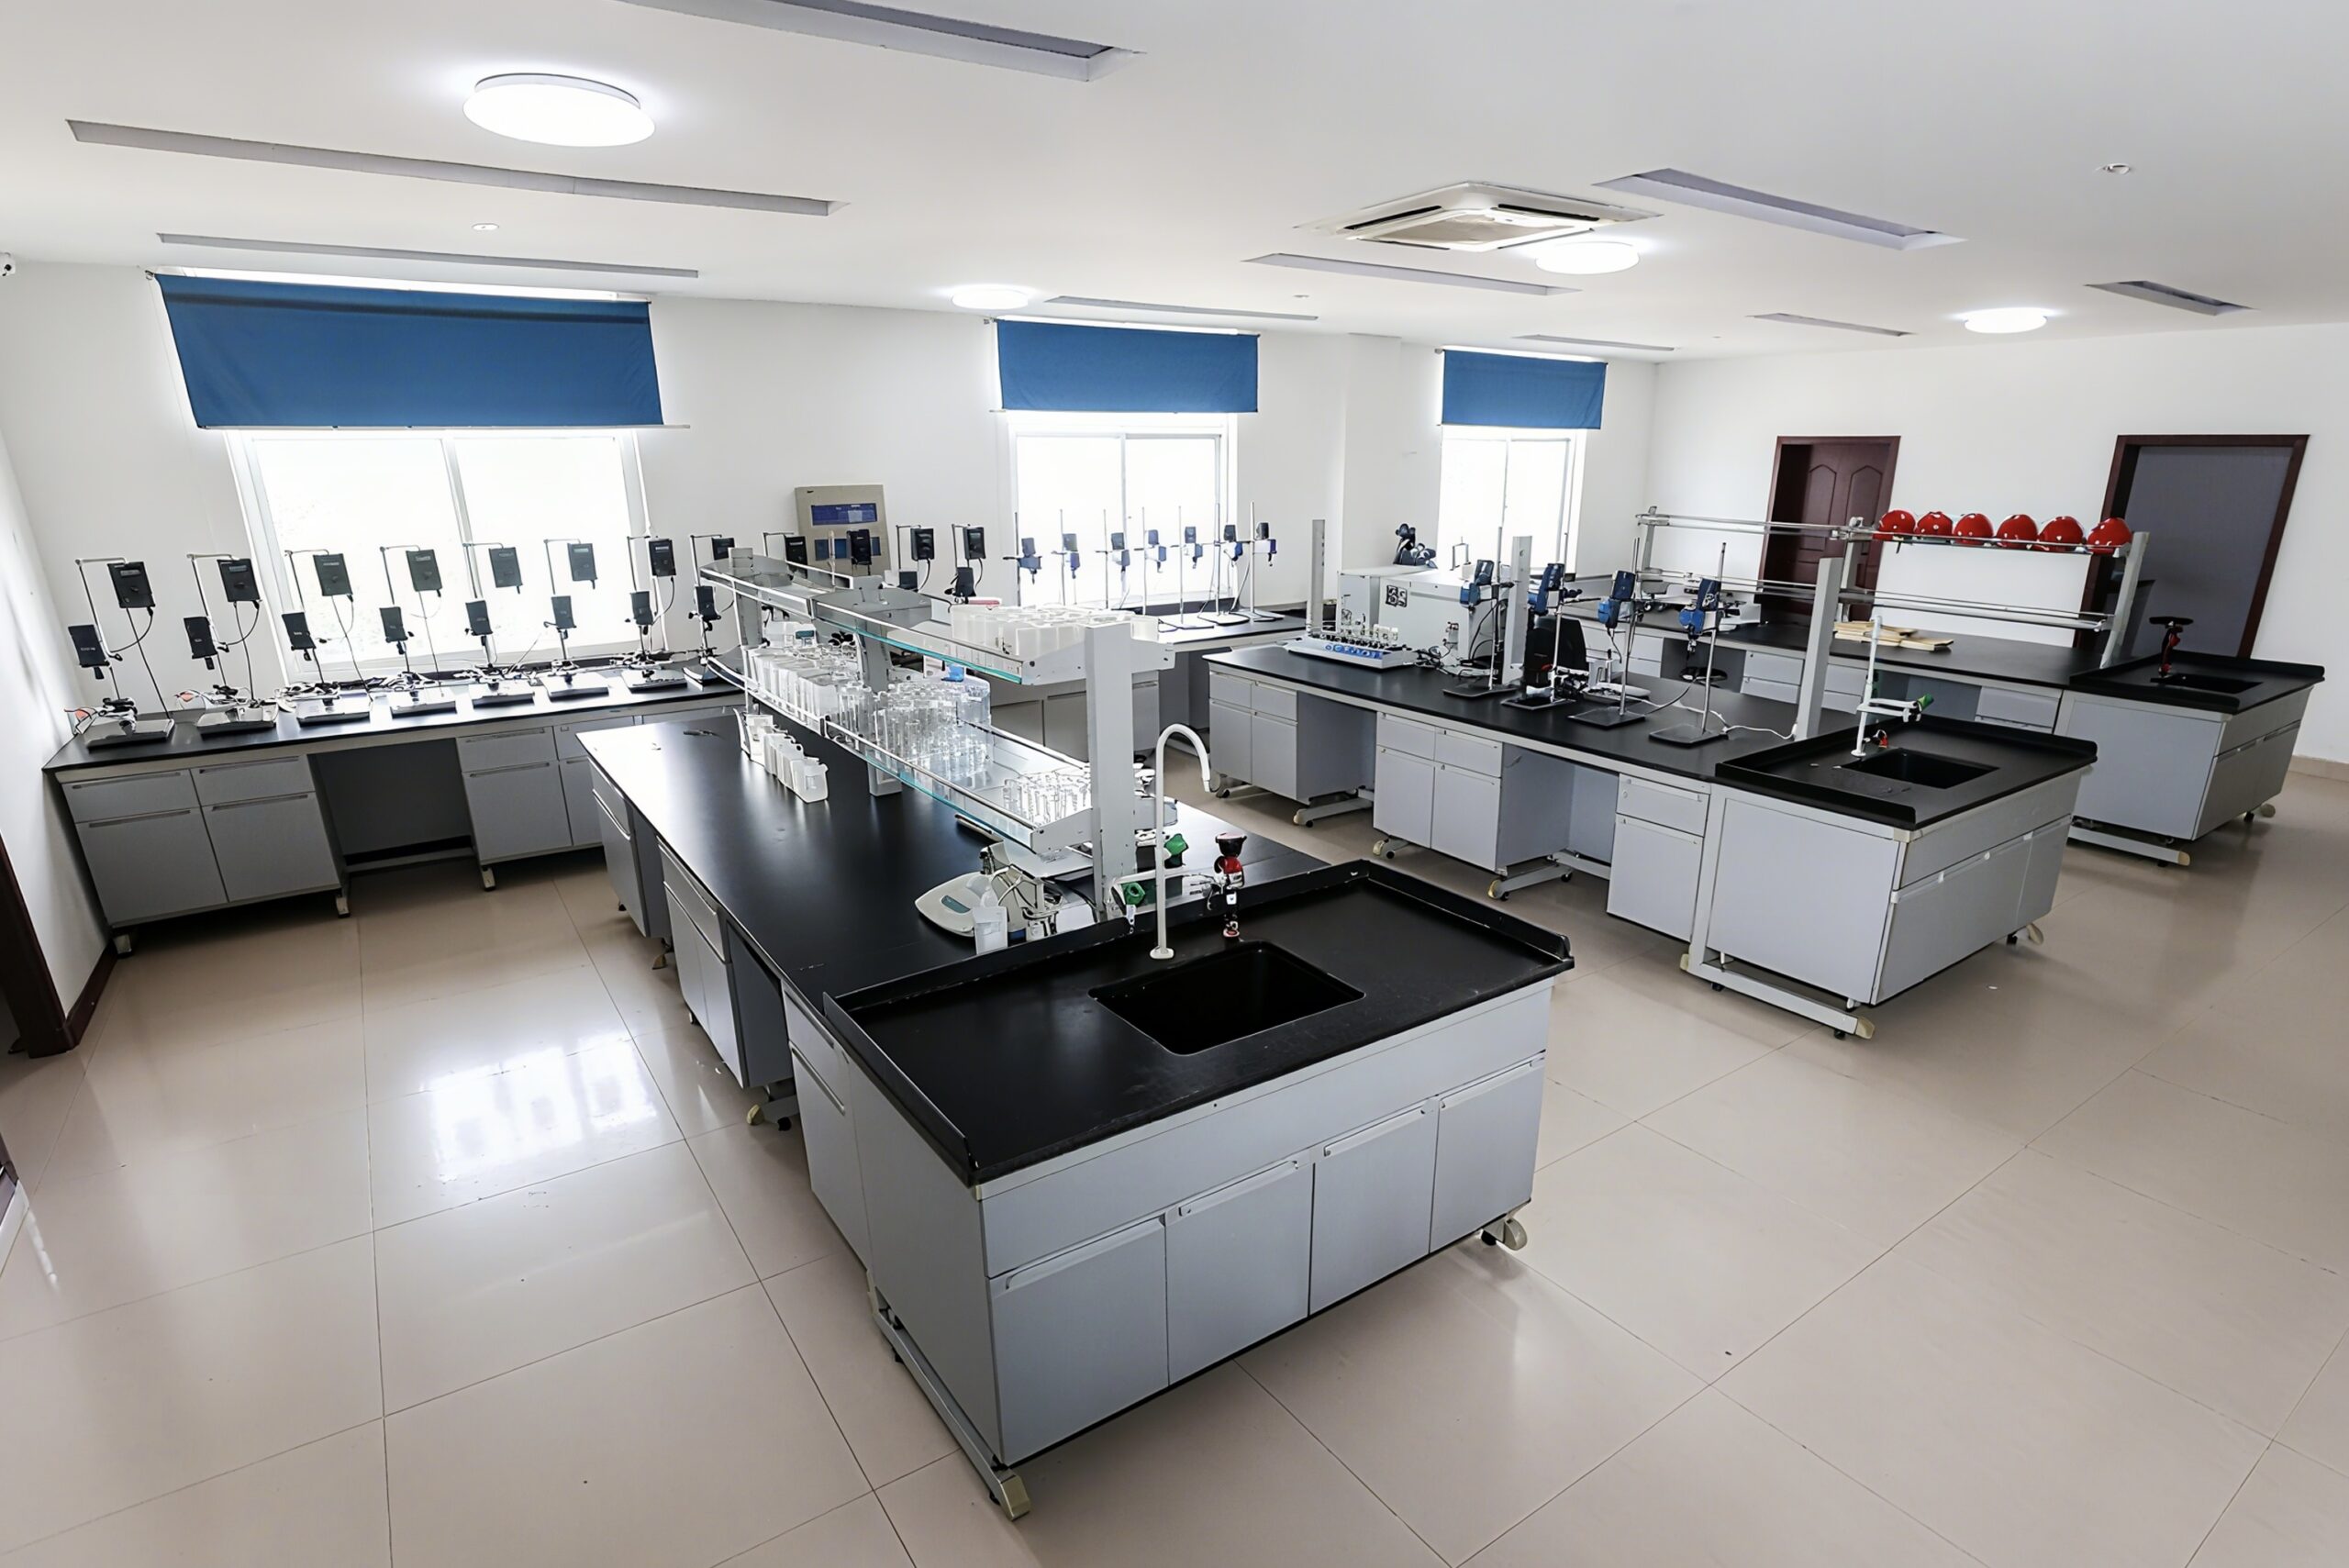
| Laboratory | Samples in progress, calibration labels on instruments, tidy retained-sample cabinet | Framed certificates only — no reagents, no raw data books |
| Retention samples & traceability | They can pull records for a lot number you pick at random | Willing to show only the most recent lot |
| Warehouse & packing | Palletised off the floor, intact liners, lots segregated and numbered | Ground-level or wall-standing storage, high bag damage rate |
10. How to read price: cost per tonne of active CMC, not price per tonne
Convert both offers into cost per tonne of active CMC before comparing. Supplier A at USD 1,700/t with 95% active costs USD 1,789/t of active material; Supplier B at USD 1,480/t with 80% active (salt or filler cutting) costs USD 1,850/t — the 13% cheaper quotation is the more expensive purchase, before you pay for blocked nozzles, scrapped batches and a stopped line.
In food, pharma and battery duty cycles, add the hidden term: one contested lot — inspection, returns, line cleaning, a customer claim — routinely costs more than the annual saving implied by the cheaper unit price.
The one-page due diligence list (send it as is)
- What is the full title and edition of the standard you manufacture to? (For food grade, GB 1886.232-2016; confirm it is the current edition.)
- Purified cotton, cotton linters or wood pulp — and what is the alpha-cellulose content?
- Can you supply COA actuals for 3–5 consecutive lots of this grade, not typical values?
- What are the test conditions for viscosity (concentration, temperature, rest period, instrument)?
- What is your in-house test list? Do you cover heavy metals and microbials? May we see calibration records?
- Certificate numbers and scope of certification (manufacturing or trading, which site, which product line)?
- Is your Halal / Kosher certification valid for our destination country, and what is the issuing body’s mutual-recognition standing with BPJPH, JAKIM or GSO?
- Annual capacity, lead time for regular grades, and how allocation works in peak season.
- Packaging specification, moisture protection and container sweat mitigation.
- Arbitration laboratory, sampling plan and response timeframe if a lot is disputed.
- Do you support plant trials, and what is your sample policy?
- Will you notify us in writing, in advance, of any change in composition, raw material or process?
About Fortune Biotech
Fortune Biotech is a cellulose ether manufacturer based in Jining, Shandong Province, China, producing CMC, PAC and related grades with an annual capacity of approximately 20,000 tonnes across food grade, pharmaceutical grade, industrial grade, drilling-fluid grade and battery grade. We are certified to ISO 9001 and ISO 14001 and hold Kosher and Halal certifications, serving more than 3,000 customers across over 60 countries.
We invite you to apply the standard above to us, including:
- starting from your application to confirm the grade, rather than from our warehouse list;
- providing consecutive-lot actuals and a hydration protocol, with support through your first plant trial;
- writing the governing standard, test conditions, sampling plan and arbitration method into the contract;
- holding regular grades to a 7–15 day preparation lead time, with complete export documentation (invoice, packing list, Certificate of Origin, Health Certificate / Free Sale Certificate) and technical files for food and Halal requirements.
If you are switching or adding a CMC supplier, send us the list above — or send your current specification along with the batch problems you’ve been fighting. We will answer it on the same terms: the exact standard we build to, consecutive-lot measured data, and samples you can verify.
Frequently asked questions
Q: What is the difference between CMC and PAC, and which one should we specify? A: Both are cellulose ethers. CMC is the economical choice and hydrates fast, covering most conventional duty. PAC carries additional anionic ether groups, giving better tolerance of calcium, magnesium and total salinity plus higher temperature stability — which is why it is usually the right answer in high-salinity brine systems and deeper, hotter sections. Select on your salinity and temperature window, not on which sounds more premium.
Q: The sample passed, but production lots don’t. How do we prevent that? A: Move acceptance upstream into the contract: governing standard, test conditions, sampling method (three-point sampling plus quartering reduction) and retention period, with the manufacturer retaining samples against every lot. For a disputed lot, send both retained samples to the agreed third-party arbitration lab. That settles arguments that email cannot.
Q: Is imported CMC still meaningfully better than Chinese CMC? A: In food, pharmaceutical and battery duty cycles the gap now shows up mainly in batch consistency, desalting depth and technical response time — not in whether a single specification can be met on paper. Leading Chinese plants are already dependable substitutes across conventional and higher-end grades. Judge on consecutive-lot data and a plant trial, not on the country of origin label.
Q: Is higher viscosity always better? A: No. Viscosity must match your process window. Too high and you fight dispersion, pumping and coating resistance, plus higher drying energy; too low and you lose thickening and suspension. Fix the target viscosity band and its permitted tolerance first, then choose the grade.